


TIG Manufacturer: OEM and Wholesale Sourcing Guide
9 月 15, 2026
Introduction
Choosing a TIG manufacturer is a supply-chain decision, not a catalogue comparison. Importers, welding-equipment brands and industrial distributors need a partner that can translate market requirements into a controlled product specification, produce repeatable batches, maintain traceable changes and support the equipment after delivery.
This guide explains how to qualify an OEM TIG manufacturer or wholesale TIG manufacturer for long-term cooperation. It covers partner models, engineering capability, compliance evidence, quotation structure, samples, pilot orders, branding, documentation, service and a practical scoring method. Use it to prepare a comparable request for quotation and to identify evidence that must be verified before volume production.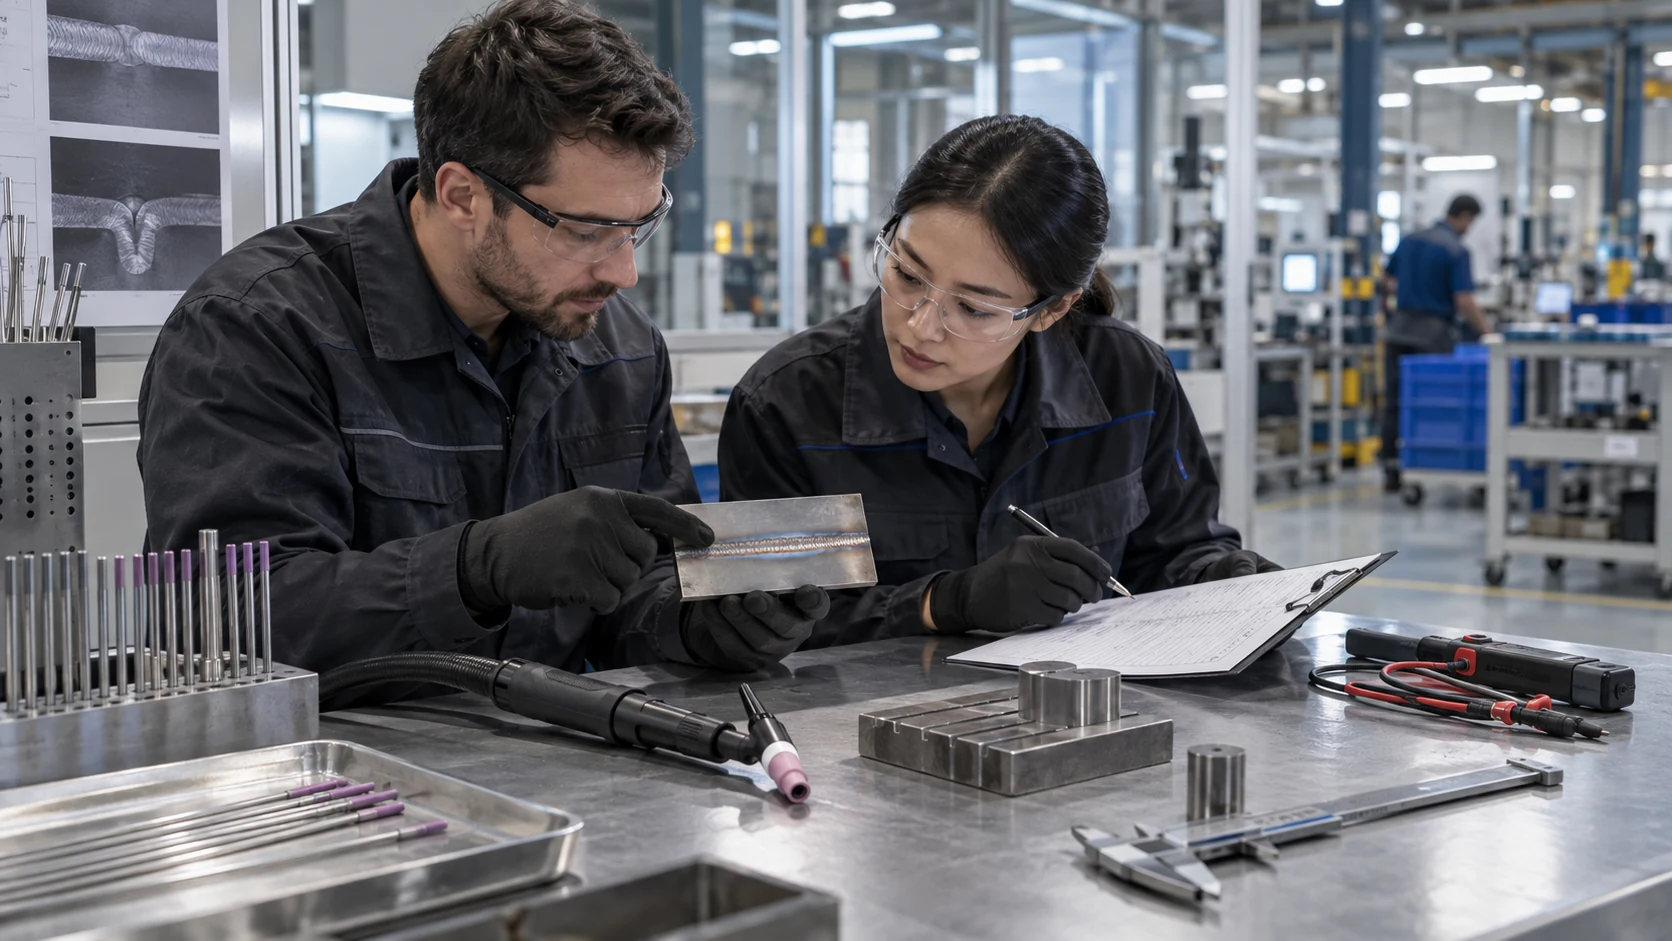
Define the Manufacturing Relationship Before Requesting Prices
Separate wholesale, private-label, OEM and ODM scope
The first decision is not machine amperage. It is the type of relationship the buyer expects. A wholesale order normally uses an existing product platform with standard hardware and limited commercial customization. Private-label supply may add the buyer’s brand, color, packaging and manuals while retaining the manufacturer’s core design. OEM work follows a buyer-controlled product specification or drawing. ODM work asks the factory to contribute product architecture, industrial design, firmware or application engineering. These models require different engineering hours, tooling, validation, minimum order quantities and ownership rules. A buyer that asks for “OEM pricing” without defining the change scope may receive quotations that cannot be compared. One supplier may quote only a logo and carton. Another may include a new panel, firmware changes, safety testing and project management.Write a responsibility matrix
Create a one-page responsibility matrix before contacting factories. Identify who owns the product requirement, mechanical files, software, tooling, certification application, labels, packaging, test plan, change approval and warranty response. State whether the buyer expects exclusive design ownership or may accept a shared platform. The matrix should also identify the markets in which the equipment will be sold and the organization responsible for importer or distributor obligations. For a faster market entry, an existing platform from a qualified wholesale TIG manufacturer can reduce development work. For differentiated controls, localized functions or a protected product line, a structured OEM or ODM project may be more appropriate. The correct model is the least complex arrangement that still meets the commercial and technical requirement.Verify Factory and Engineering Capability
Confirm which work is performed in-house
A supplier’s website may show finished machines without explaining who designed, assembled or tested them. Ask for a process map covering incoming inspection, electronic assembly, power-stage assembly, firmware loading, calibration, functional testing, load testing, final inspection and packing. Identify processes performed by subcontractors and the controls used for those suppliers. The purpose is not to demand that every operation occur under one roof. It is to understand responsibility and change control. If a key printed circuit board assembly, transformer, enclosure or software module is outsourced, the manufacturer should still control specifications, incoming acceptance, revisions and nonconforming material.Test engineering communication with a real requirement
Send a representative application instead of asking whether the factory can make “high quality” equipment. Include base materials, thickness range, input supply, expected current range, duty pattern, torch cooling, control functions, target markets and annual volume. A capable engineering team should identify missing information, explain platform limits and separate standard features from development work. Ask who will approve the specification and who can answer questions during sampling. Distributor sales teams need a named technical path because commercial contacts may not control firmware, electrical design or test criteria. Evaluate response quality as well as response speed. A useful answer identifies assumptions and evidence; a fast yes without boundaries creates risk.Review design and change-control records
For OEM cooperation, request the document list used to release a model: bill of materials, drawings, firmware version, parameter table, inspection standard, test procedure and approved sample. Ask how engineering changes are numbered, reviewed and communicated. The buyer should receive advance notice when a component, supplier, enclosure, control board or software revision can affect fit, function, compliance or service parts. GWELD presents OEM and ODM support through in-house product definition, engineering, prototyping and batch-production stages. Buyers can review the company’s OEM manufacturing capabilities and then request project-specific evidence for the exact platform under consideration.Translate Market Needs into a Controlled Product Specification
Define the application envelope
A quotation should start from the jobs the machine must perform. Record material families, thicknesses, joint types, weld positions and expected production pattern. State whether the range requires DC TIG, AC/DC TIG, pulse functions, stick capability, remote control or water cooling. Separate mandatory functions from preferences so the factory can propose a compliant base configuration without hiding necessary options. Input power deserves its own line. Specify voltage, phase, frequency, plug or cable requirement and the markets where the model will be sold. Do not assume that one universal input design is commercially or technically suitable everywhere. The specification should include nameplate information, manual language and packaging labels for each destination.Set measurable performance and interface requirements
Maximum amperage alone is not an acceptance criterion. Define the useful current range, starting method, duty-cycle point, output control tolerance, required pulse range and any AC balance or frequency functions. Specify the torch and cooling arrangement as part of the system. If the product must integrate with automation, identify the required analogue, digital or remote signals and the responsibility for interface validation. For product-platform decisions, compare these requirements with the GWELD TIG welder range. Buyers that still need to define the operating window can use the industrial TIG welder selection guide before sending the RFQ.Control accessories and deliverables
List the complete delivered configuration: power source, torch, ground lead, electrode holder, remote device, gas equipment, water cooler, hoses, starter consumables, power connection, manuals and spare parts. Identify acceptable substitutions. A low unit price can become expensive when required accessories, destination plugs, replacement connectors or commissioning support are excluded. For pulse-specific controls, production evidence and a factory acceptance checklist, use the pulse TIG welder manufacturer buying guide when finalizing the RFQ.Audit Quality, Compliance and Traceability Evidence
Verify the quality system behind the certificate
A quality certificate is a starting point, not a substitute for process evidence. The official ISO 9001 overview describes a quality-management framework built around controlled processes, performance evaluation and continual improvement. Ask for the certificate scope, issuing body, covered site and validity, then compare that scope with the factory and product being quoted. During a remote or on-site audit, trace one model from incoming material through assembly, test and shipment. Review how the factory controls inspection status, calibration, training, nonconforming products, corrective actions and approved suppliers. Sample records should contain identifiable dates, models or batch references rather than generic forms prepared only for a sales presentation.Request product-specific safety and performance evidence
这 IEC 60974-1 standard applies to industrial and professional arc-welding power sources within its stated scope and specifies safety and performance requirements. The buyer should ask which standards and editions apply to the proposed model, which laboratory or internal facilities performed the tests and whether reports match the exact electrical and mechanical configuration. For products intended for the European Economic Area, the European Commission explains that the manufacturer is responsible for the applicable conformity assessment, technical documentation, EU declaration of conformity and CE marking. A CE logo on a photograph is not the complete evidence. Request the declaration, applicable legislation and standards list, model identity and supporting technical file process. Importers and distributors should also confirm their own obligations for the target market.Build serial and component traceability into the order
Define how finished machines are linked to production date, test result and material or component batches. For critical electronic assemblies, agree which component changes require buyer notification. An open bill of materials may not be appropriate for every commercial relationship, but the buyer still needs controlled part numbers, approved alternatives and service compatibility. Ask for the final-test record format and the retention period. For recurring orders, compare failure and repair information by batch rather than treating every event as an isolated complaint. Traceability makes root-cause analysis faster and prevents a corrective action on one revision from being applied incorrectly to another.
Compare MOQ, Samples, Pricing and Contract Terms
Separate one-time costs from recurring unit costs
An OEM TIG manufacturer quotation may contain engineering fees, tooling, certification work, packaging setup and sample costs in addition to the production price. Put these items in separate columns. State whether each fee is refundable, amortized, reusable for later orders or owned by the buyer. A lower unit price can hide a large setup cost; a higher unit price may include accessories, testing or documentation that another quotation excludes. Ask for price breaks at realistic annual volumes, but do not use an optimistic forecast to obtain a number the buyer cannot maintain. Compare the price of the complete approved configuration at the same Incoterm, currency, payment structure and validity period. Keep freight, import charges, certification, samples and spares visible instead of blending them into one unexplained total.Understand what drives MOQ
Minimum order quantity can be driven by enclosure production, custom colors, printed packaging, front-panel overlays, transformers, circuit boards or supplier pack sizes. Ask the factory to separate the MOQ for standard products, logo customization, custom packaging and engineering changes. This allows the buyer to stage the project. A standard-platform pilot may be possible before committing to the MOQ for custom housings. For wholesale programs, ask whether mixed-model orders, spare-parts kits or consolidated shipments are allowed. A wholesale TIG manufacturer should explain carton quantities, production lead times and the conditions for repeat-order pricing. Record whether a quoted lead time begins at deposit, artwork approval, approved sample or receipt of components.Use a quotation-normalization table
| Commercial item | Supplier response required | Buyer check |
|---|---|---|
| Base configuration | Model, input, output and included accessories | Matches controlled specification |
| 定制 | Logo, color, panel, firmware, packaging and manuals | Scope and approval owner defined |
| One-time charges | Engineering, tooling, artwork and compliance work | Ownership and reuse terms stated |
| MOQ and price breaks | Quantity by customization level | Based on realistic order plan |
| Lead time | Sample and production milestones | Start event and dependencies clear |
| Payment and delivery | Currency, payment stages and Incoterm | Same basis across suppliers |
| Warranty and service | Period, exclusions, parts and claim process | Destination support is workable |
Validate Samples and a Pilot Order
Approve the golden sample against a written plan
A sample is useful only when it represents the proposed production configuration. Record the model, serial number, hardware revision, firmware or parameter version, torch, cooler, accessories, labels and packaging. The test plan should cover input supply, functions, output range, repeated arc starts, duty pattern, alarms, thermal behavior and representative weld trials. Use actual materials and joint conditions where practical. Record settings, tungsten, filler, gas, operator and inspection method. Photographs of an attractive bead do not replace a repeatable acceptance record. If the sample requires a workaround or different accessory, document it and update the quotation before approval.Use a pilot order to test the supply process
A golden sample proves one unit. A pilot order tests purchasing, production, inspection, packing, documentation and delivery as a system. Select a quantity large enough to expose batch controls but small enough to limit risk. On receipt, inspect model identity, accessories, appearance, labels, manuals and packing before functional testing. Track discrepancies in one closure list with owner, action and due date. Do not allow verbal approval of changes to replace the controlled specification. Before the first volume order, update drawings, bills of material, packaging files, test criteria and approved sample references so every party is working from the same release.Define pass, conditional pass and fail
A pass means all mandatory requirements are met in the quoted configuration. A conditional pass lists specific corrective actions or approved restrictions and requires closure evidence. A fail identifies the unmet requirement and whether retesting is permitted. This language prevents delivery pressure from turning an unresolved sample issue into an informal production standard.Plan Branding, Documentation and After-Sales Support
Control brand assets and market documents
Provide controlled logo files, colors, model naming, rating-label content, carton marks and manual languages. Define who approves artwork and how revisions are recorded. Check that the product identity is consistent across the machine, carton, declaration, manual, warranty record and spare-parts list. A mismatch can create customs, service and customer-support problems. Localized manuals should cover safe setup, operating controls, maintenance, troubleshooting and the supplied configuration. Machine translation without technical review can change electrical or safety meaning. Assign review responsibility to people who understand both the language and the equipment. Keep editable source files and the final released PDF under revision control.Design the service model before launch
Decide whether the distributor, manufacturer or an authorized partner handles diagnosis and repair. Request troubleshooting flowcharts, fault-code information, wiring diagrams where appropriate, parts lists and training material. Define which components the distributor may replace, which require return-to-factory service and how warranty authorization is obtained. Build an initial spare-parts package from expected failure modes, installed quantity and replenishment lead time. Include torches and consumables separately from machine components. Agree on part-number stability and substitution notice. A low purchase price loses value when one connector, board or display cannot be identified or supplied.Measure supplier performance after shipment
Use a small scorecard for on-time delivery, incoming defects, functional failures, documentation errors, response time and corrective-action closure. Normalize failure rates by shipped or installed units and keep the observation period visible. Share evidence with the factory and separate confirmed causes from initial symptoms. The objective is process improvement, not a one-time negotiation.Score TIG Manufacturers with a Decision Matrix
Pass mandatory gates before applying weights
Do not let a low price offset a failed safety, electrical or application requirement. Mark mandatory gates first: process fit, input compatibility, required functions, applicable compliance evidence and acceptance testing. Only suppliers that pass those gates should enter a weighted commercial comparison. Weights should reflect the business model. A private-label distributor may give more weight to customization, documentation and warranty support. A factory buying standardized production equipment may emphasize duty-cycle evidence, parts availability and fleet consistency. Record the evidence behind every score and use the same scoring definitions for all candidates.| Evaluation area | Example evidence | Typical decision question |
|---|---|---|
| Application fit | Controlled specification and weld trial | Does the proposed configuration meet every mandatory job? |
| Engineering capability | Design records, named technical contact and change process | Can the factory resolve and control technical changes? |
| Quality system | Certificate scope, audit trail and corrective actions | Are recurring batches produced under controlled processes? |
| Compliance | Model-specific reports, declaration and technical-file process | Is the evidence valid for the product and destination? |
| Commercial model | Normalized quotation, MOQ and lead-time basis | Is total landed and lifecycle cost clear? |
| Service | Warranty workflow, spares and training | Can the buyer restore equipment to service predictably? |
| Supplier capacity | Production plan and delivery history | Can the partner support forecast and growth without losing control? |
Compare risk and price separately
Present the compliant price and the residual risks in adjacent fields. Examples include a single-source component, unverified localized manual, long spare-part lead time or pending packaging validation. Assign owners and closure dates rather than hiding risks inside a blended score. Management can then decide whether the price difference justifies the remaining exposure. For a deeper technical benchmark, compare this commercial framework with the existing heavy-industrial TIG manufacturer guide and the industrial OEM manufacturer guide. Those resources focus on power-source architecture and factory engineering, while this article focuses on partnership and sourcing control.Prepare a Comparable RFQ and Factory Audit Checklist
Send one controlled RFQ package
Issue the same package to every shortlisted supplier. Include the application envelope, electrical markets, mandatory functions, expected annual volume, sample quantity, customization scope, documentation languages, compliance responsibilities, accessories, spares, warranty expectation and target schedule. Ask suppliers to list every deviation instead of silently substituting their standard configuration.- Confirm the legal manufacturer, factory location and responsible technical contact.
- Define wholesale, private-label, OEM or ODM scope and ownership.
- Attach the controlled product and accessory specification.
- Request quality-system scope and model-specific compliance evidence.
- Separate samples, tooling, engineering and recurring production pricing.
- State the required sample, pilot and production acceptance process.
- Request lead-time milestones, MOQ basis and change-notification rules.
- Define manuals, labels, packaging, spare parts and warranty workflow.
- List commercial assumptions, exclusions and quotation validity.
- Require a deviation schedule signed off before order placement.
Use the audit to verify the quotation
The factory audit should test whether the quoted process exists and is used. Select records from normal production, trace a product through inspection and ask operators to explain the current work instruction. Compare observed part numbers, test equipment and documents with the quotation. Record evidence, open items and owners. A polished tour is not a substitute for a traceable process. GWELD supports international distributors and industrial buyers with standard platforms and OEM/ODM development. Send the target market, material range, input power, functions, order volume, branding scope and compliance needs through the GWELD technical inquiry team to request a configuration and itemized quotation.Related Products

TIG 315/350P ACDC
A compact, air-cooled TIG/Stick inverter welder designed for AC and DC welding.
- 适用于饮水机.
- 采用更坚固耐用的材料。.
- 配备精选且可靠的附件,以提升焊工的体验。.
- 工业级焊机采用更高的冗余设计,可提高可靠性、延长使用寿命并增强耐用性。.

TIG 300/400/500 直流脉冲
A compact, air-cooled TIG/Stick inverter welder designed for AC and DC welding.
- 使用更坚固耐用的材料
- 适用于饮水机.
- 配备精选且可靠的附件,以提升焊工的体验。.
- 工业级焊机采用更高的冗余设计,可提高可靠性、延长使用寿命并增强耐用性。.
TIG 180/200/225P ACDC
A compact, air-cooled TIG/Stick inverter welder designed for AC and DC welding.
- 专为铝焊设计,精确控制细薄易损材料。.
- 先进的脉冲技术有助于减少热输入并改善焊缝外观。.
- 采用耐用组件和坚固结构,确保长期可靠性。.
相关解决方案

重型制造
重工业严苛需求的终极TIG焊机解决方案。我们的设备采用坚固的材料和周到的研发,可提供高强度不锈钢接头所需的精确控制,以及厚碳钢深层熔透所需的可靠动力。体验专业性能,平衡设计,专为最苛刻的制造环境而打造。.


Frequently Asked Questions
Conclusion
The right TIG manufacturer is the partner that can convert commercial requirements into a controlled product, prove repeatable production and support the equipment throughout its market life. Define whether the project is wholesale, private label, OEM or ODM before comparing prices. Then verify engineering ownership, quality controls, compliance evidence, samples, pilot production, documentation, spares and warranty response.
Use mandatory gates before weighted scoring, and compare complete quotations on the same commercial basis. For a GWELD project review, send your destination markets, electrical supply, welding applications, required functions, estimated volume and branding plan to the GWELD OEM and wholesale team.


