TIG Welding Gas: Argon, Flow Rate & Gas Lens Guide
Introduction
TIG welding gas shields the tungsten electrode and weld pool from air. Pure argon is a common starting choice for TIG welding steel, stainless steel and aluminum; other mixtures need material-specific procedure approval.
For TIG welding gas flow rate, about 15–20 CFH (7.1–9.4 L/min) is a practical starting range for many indoor setups, not a universal setting. Confirm the torch manual, cup size, gas lens, electrode extension and drafts, then validate shielding on a representative weld.
Which Gas Is Used for TIG Welding?
Pure argon for common applications
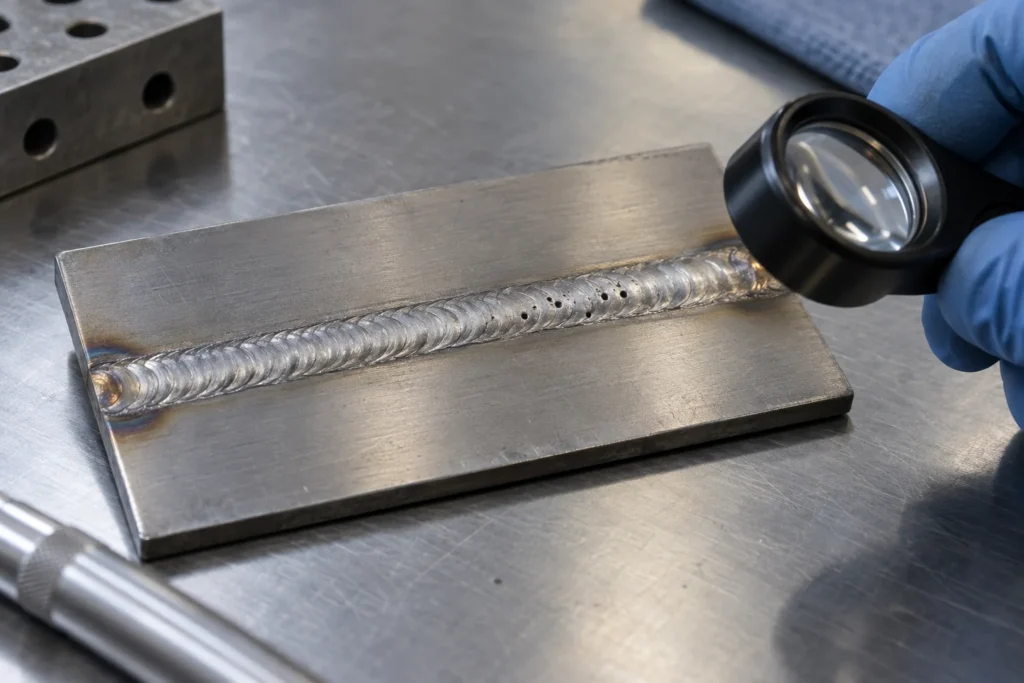
Pure argon is widely used for TIG welding carbon steel, stainless steel and aluminum. It provides a stable arc, but gas choice alone cannot prevent porosity: surface cleanliness, leaks, drafts and torch technique also matter.
Mixtures require procedure approval
Argon–helium mixtures may be considered where additional heat input is needed. Hydrogen-containing mixtures are not general-purpose substitutes and require alloy-specific procedure approval. Do not substitute a MIG shielding mixture containing carbon dioxide or oxygen without a qualified TIG procedure.
Review material-specific considerations in our guides to 氩弧焊铝, TIG welding stainless steel 和 TIG welding copper.
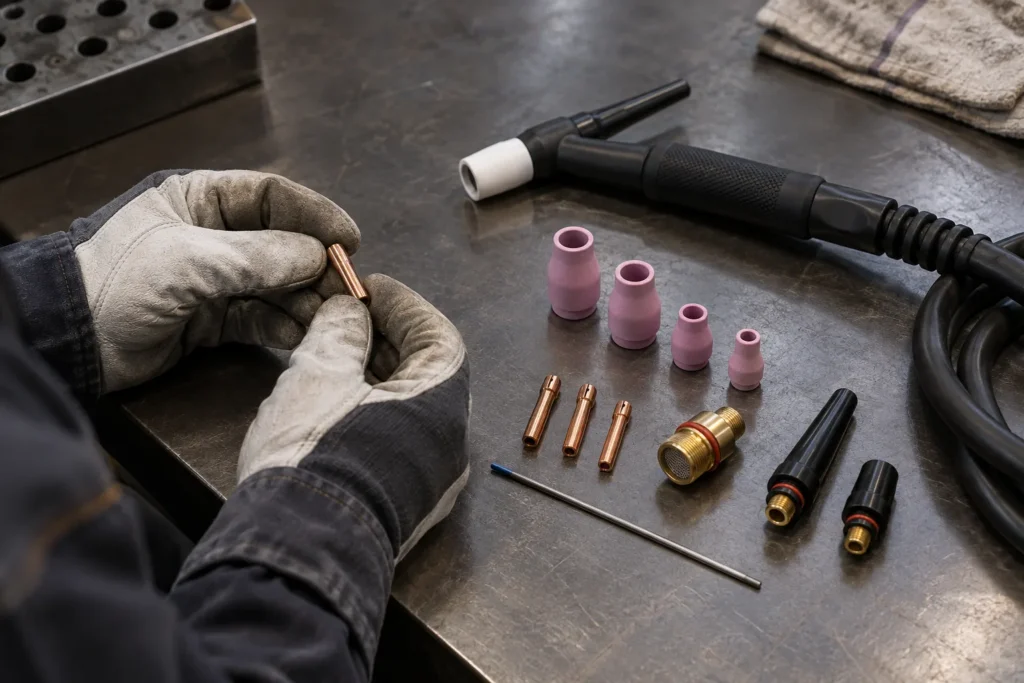
TIG Welding Gas Lens vs. Standard Collet Body
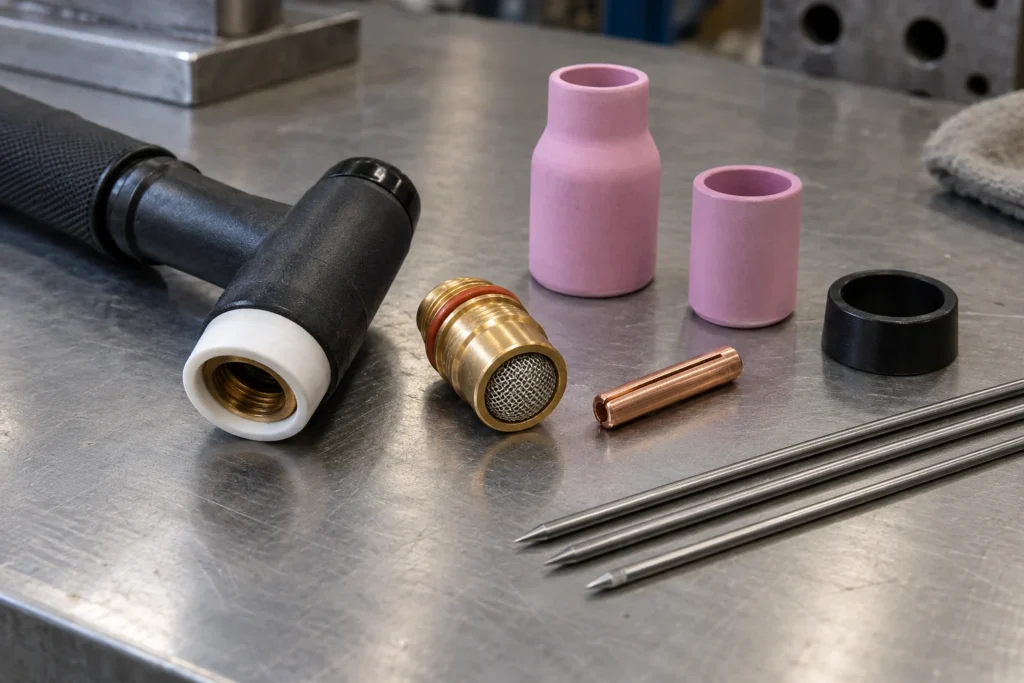
A TIG welding gas lens uses mesh screens to help distribute shielding gas more evenly than a conventional collet body. It can improve access where additional electrode extension is needed, but permitted extension and flow depend on the complete torch setup.
- Check fit: torch series, collet, electrode diameter, insulator and cup must match.
- Validate coverage: test the actual cup, electrode extension and joint; a larger lens does not guarantee freedom from contamination.
- Measure savings: compare gas used per accepted weld rather than assuming a fixed saving percentage.
Use our gas lens fit and procurement guide 和 TIG torch parts guide before ordering spares.

TIG Welding Gas Flow Rate: CFH and L/min
A starting range of 15–20 CFH (7.1–9.4 L/min) is commonly suggested for many TIG setups. Manufacturer guidance varies; use the torch manual and qualified welding procedure to set the final value. More gas is not always better, because excessive flow may disturb shielding.
Gas flow unit conversion chart
| Flow (CFH) | Approx. L/min | How to use this value |
|---|---|---|
| 10 | 4.7 | Conversion only; not a universal welding setting |
| 15 | 7.1 | Common starting-range reference |
| 20 | 9.4 | Common starting-range reference |
| 25 | 11.8 | Confirm the actual torch and shielding requirement |
| 35 | 16.5 | Not an automatic cure for porosity |
Conversion basis: 1 CFH ≈ 0.472 L/min. These rounded conversions do not specify the correct flow for a particular cup or alloy.
Before increasing gas flow
- Check cylinder contents, gas-specific flowmeter calibration and hose connections.
- Measure flow with gas running; inspect leaks, cup damage and blocked screens.
- Control drafts and confirm electrode extension, arc length, preflow and postflow.
- Run a representative sample and assess it against the applicable acceptance criteria.
See Miller’s TIG troubleshooting guidance for the starting-flow context. For equipment selection, review our industrial TIG machine buying guide.
Flow rate and gas duration are separate controls. Use our TIG pre-flow and post-flow setup guide to document the start-and-stop sequence, torch-hold behaviour and sample acceptance before transferring settings into production.
Shielding Setup Comparison: What to Validate
Compare shielding hardware using evidence from the actual process, not guaranteed defect rates.
| Setup | Potential use | Required validation |
|---|---|---|
| Standard collet body | Routine access and compact assemblies | Cup size, gas distribution and allowable extension |
| Standard gas lens | More even gas distribution and restricted joint access | Torch fit, screen condition, actual flow and weld acceptance |
| Large gas lens | Wider shielding coverage where the procedure requires it | Access clearance, coverage, trailing shielding and gas consumption |
No setup guarantees zero contamination or a particular NDT pass rate. Record the gas specification, flow, electrode extension, inspection results and gas consumption for each trial.
Illustrative Shielding Validation Workflow
This is an illustrative qualification workflow, not a documented customer case or a performance guarantee. Reactive materials and high-specification joints need procedure-specific shielding and inspection requirements.
- Define the alloy, joint geometry, applicable welding procedure and acceptance criteria.
- Verify gas certification, supply cleanliness, leakage control and required torch, trailing or backing shielding.
- Document the torch setup, flow measurement, preflow and postflow used in a representative trial.
- Assess the trial using the required inspection method; qualify the process before fleet rollout.
- Measure accepted output, gas consumption and rework over a controlled production sample.

Related Products

TIG 180/200/225 直流脉冲
A compact, air-cooled TIG/Stick inverter welder designed for AC and DC welding.
- 采用耐用的内部组件和加固结构,确保长期可靠性。.
- 支持TIG脉冲和焊条焊接不锈钢、碳钢、铜及其他常见金属。.
- 紧凑便携的设计,适用于车间、车库、移动维修和日常制造工作。.

TIG 180/200/225P ACDC
A compact, air-cooled TIG/Stick inverter welder designed for AC and DC welding.
- 专为铝焊设计,精确控制细薄易损材料。.
- 先进的脉冲技术有助于减少热输入并改善焊缝外观。.
- 采用耐用组件和坚固结构,确保长期可靠性。.
TIG 300/400/500 直流脉冲
A compact, air-cooled TIG/Stick inverter welder designed for AC and DC welding.
- 使用更坚固耐用的材料
- 适用于饮水机.
- 配备精选且可靠的附件,以提升焊工的体验。.
- 工业级焊机采用更高的冗余设计,可提高可靠性、延长使用寿命并增强耐用性。.

TIG 315/350P ACDC
A compact, air-cooled TIG/Stick inverter welder designed for AC and DC welding.
- 适用于饮水机.
- 采用更坚固耐用的材料。.
- 配备精选且可靠的附件,以提升焊工的体验。.
- 工业级焊机采用更高的冗余设计,可提高可靠性、延长使用寿命并增强耐用性。.

TIG 400/500P ACDC
A compact, air-cooled TIG/Stick inverter welder designed for AC and DC welding.
- 适用于饮水机.
- 采用更坚固耐用的材料。.
- 配备精选且可靠的附件,以提升焊工的体验。.
- 工业级焊机采用更高的冗余设计,可提高可靠性、延长使用寿命并增强耐用性。.
相关解决方案

管道
专为关键管道制造和现场管道施工而设计的终极 TIG 焊机解决方案。我们采用深思熟虑的研发驱动,并使用重型实心材料制造,我们的机器可提供对不锈钢完美 5G/6G 起始焊缝所需的精确电弧控制,以及对碳钢管道深熔填充焊缝所需的可靠动力。通过专为世界上最苛刻的能源和工艺管道项目而设计的平衡设计,实现 X 射线质量的接头和最大的正常运行时间。GWELL 确保您的团队始终能够提供专业性能,消除昂贵的现场返工。.

海上
终极 TIG 焊机解决方案,适用于最严苛的海洋环境。我们的机器采用坚固的材料和周密的研究与开发制造,能够承受潮湿和盐雾,同时提供精密电弧控制,满足关键海上基础设施的需求。在一个平衡的设计中体验专业性能,即使在浮动平台或偏远船厂也能保持可靠——确保您在任务关键时始终做好准备。.


Conclusion: Specify the Complete Shielding System
Reliable TIG welding gas performance depends on the gas, delivery system, torch consumables and welding procedure working together. Validate settings on representative parts rather than accepting universal flow values or unsupported pass-rate claims.
For a matched equipment discussion, send the alloy, thickness, joint type, torch series, cooling method and duty pattern to the GWELD equipment consultation team. Ask for model-specific documentation and trial requirements before procurement.