DC TIG Welder Manufacturer: Sample Acceptance Guide
Introduction
A DC TIG welder manufacturer should demonstrate that the quoted machine can start, regulate and stop the arc reliably on your actual steel or stainless steel jobs. Select the supplier through a documented sample-acceptance plan that connects the application, electrical supply, accessories and inspection results to one identified product configuration.
This guide gives industrial buyers a practical way to qualify that configuration before ordering a batch. It focuses on DC process suitability, low-current behavior, duty-cycle evidence, control interfaces and release records. It does not claim that a catalogue rating or a good-looking sample weld proves every production requirement.
When Does a DC TIG Welding Machine Fit the Job?
A DC TIG welding machine is a sensible starting point for many steel and stainless steel applications when its current range, controls and accessories match the work. Establish material and joint requirements before comparing suppliers. A DC-only purchase needs a clear boundary when the same workshop also plans to weld aluminum.
Separate the welding process from the incoming supply
DC describes welding output, not whether the equipment plugs into an AC electrical supply. Record the required input voltage, phase and frequency separately from welding polarity. Confusing these two specifications can result in a machine that has the desired welding functions but cannot be installed as intended.
Miller's TIG basics guide distinguishes DC capability for steel and stainless from AC/DC selection for aluminum versatility. Use this as general process guidance, not as evidence of another manufacturer's model performance. Specialized DC aluminum procedures require separate engineering evaluation and are outside this purchase checklist.
Write the application boundary into the order
List base-metal grades, thickness range, joint design, weld positions and access restrictions. Identify whether the job needs manual filler addition, autogenous welding or an integrated feeder. Refer aluminum requirements to the AC TIG equipment selection guide rather than treating DC pulse as a substitute for AC output.
What Should the Supplier Receive Before Quoting?
Send every candidate the same application sheet and require a written deviation list. A useful quotation identifies the complete delivered system and the tests it will undergo. This keeps an inexpensive power source from being compared with a fully equipped welding package whose torch, cooler and controls are already included.
Define the production task
-
- Material grades, representative thicknesses and joint drawings.
- Expected current window and the actual weld-and-pause sequence.
- Available input supply, installation location and ambient conditions.
- Required start method, trigger sequence, remote control and pulse functions.
- Torch cooling, cable reach, gas equipment and spare consumables.
- Destination market, documentation language and planned order quantity.
Include photographs or drawings of difficult access points. Distinguish an absolute requirement from a preference, and name the person who can approve a deviation. If an installation condition remains unknown, flag it as an open input instead of allowing the supplier to choose an unrecorded assumption.
Request comparable scope
Separate standard equipment, options, development work, sample cost and repeat-order pricing. The existing OEM and wholesale sourcing framework covers the broader commercial relationship. The checklist here adds DC-specific acceptance evidence rather than repeating a general factory audit.
Freeze the Sample Identity Before Testing
Identify the sample and all supporting equipment before recording a test result. Approval applies to that configuration, not automatically to every unit carrying a similar model name. A TIG factory acceptance test loses value when firmware, input variant, torch or remote control changes between the demonstration and the delivered batch.
Create a configuration cover sheet
Record model designation, serial number, nameplate photograph, hardware revision where available, firmware or parameter version, input variant and accessory part numbers. Attach the manual revision and supplier quotation. Use the same sample identifier on photographs, measurement files and inspection reports so an independent reviewer can connect the records.
Agree which substitutions require approval. A connector revision, different pedal or alternative torch may change function even when the power-source enclosure looks identical. Label the retained reference sample and record its storage location and condition. Do not rely on a salesperson's photograph to identify a production release.
Separate product approval from process qualification
Equipment acceptance checks whether the quoted system meets the purchase specification. A qualified welding procedure, operator approval and project inspection remain separate requirements where applicable. Passing this buying checklist does not certify a weld, pressure component or regulated production process.
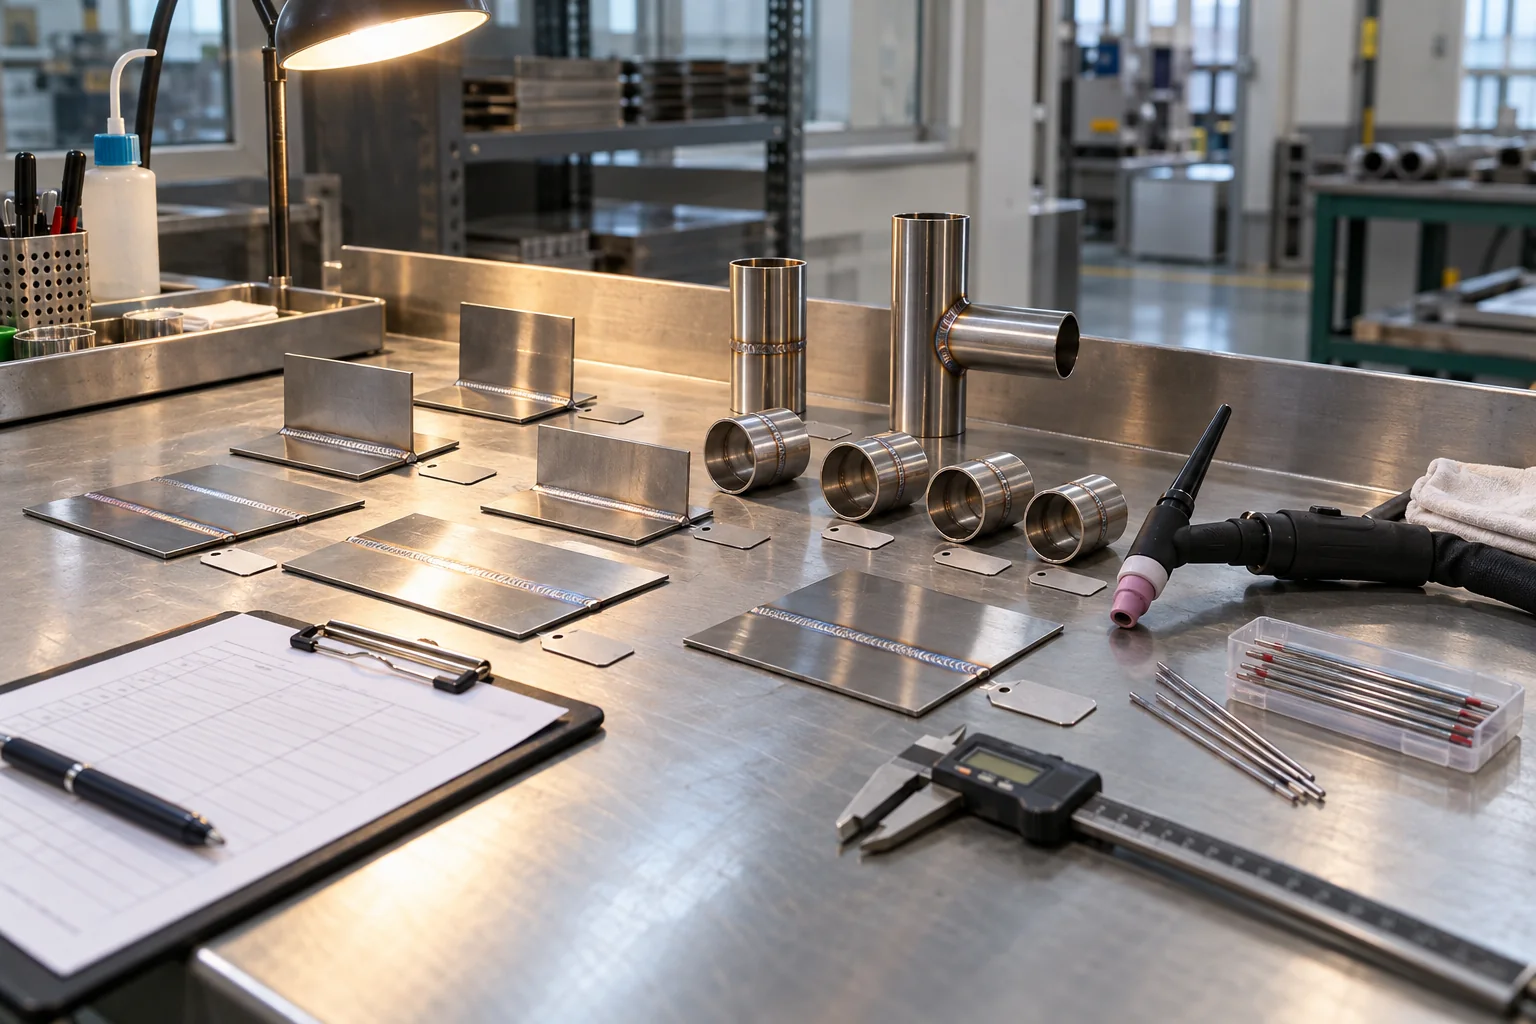
AI-generated illustration of a sample-inspection workbench, not an actual GWELD factory test.
How Do You Check Low-Current Starts and Arc Control?
Evaluate low-current performance using your thinnest representative joint and the supplied start method. Minimum displayed amperage alone cannot show how consistently the arc starts or whether the operator can control the first part of the weld. Agree the trial conditions and acceptance criteria before the supplier demonstrates the sample.
Record starts rather than selecting the best bead
Use identified coupons and a written sequence of repeated starts, short welds and stops. Record commanded current, starting mode, electrode preparation, torch arrangement and any failed ignition, electrode sticking or unexpected current surge. Choose the trial count with the welding engineer and apply the same sequence to each candidate.
Where the machine offers both HF and Lift TIG, verify the quoted modes individually. Do not assume a remote trigger or pedal behaves the same in every mode. Review the HF and Lift TIG comparison when defining the starting requirement, especially for work where contact with the coupon is undesirable.
Check the whole start-to-stop sequence
Observe the transition from starting current to working current, downslope, crater current and gas timing where provided. Test after the system has warmed during normal operation as well as from its initial condition. Record deviations without adjusting several variables at once, then retest the agreed correction.
Read Duty-Cycle Ratings Without Overbuying Amperage
Compare an industrial DC TIG welder at the current and conditions your work actually needs. A maximum-current number without its duty cycle, load voltage, input conditions and stated ambient basis is incomplete. Ask for the rating table and supporting evidence rather than accepting a broad continuous-output claim.
Keep the rating conditions visible
Lincoln Electric's operator-manual explanation of duty cycle uses the share of a ten-minute period at rated welding current. On that basis, a 60% example means six minutes of welding and four minutes without welding. This explains the notation only; it is not a claimed GWELD rating or a test prescription.
| Rating information | Supplier response needed |
|---|---|
| Required operating point | Output current and rated load voltage for the intended job. |
| Duty-cycle basis | Percentage, reference period and stated ambient condition. |
| Input variant | Voltage, phase, frequency and installation requirements. |
| Thermal behavior | Documented protection and recovery behavior within the manual. |
| System limit | Torch, cable and cooler limits as well as power-source capability. |
Validate the real work pattern safely
Have qualified personnel compare the proposed rating with the planned weld-and-pause sequence using an approved test plan. Keep ventilation clear and remain within the equipment instructions. Never defeat thermal protection or improvise exposed electrical measurements to prove a sales claim. A sample trial does not replace standardized type testing.
Verify Pulse, Remote Controls and Automation Interfaces
A DC pulse TIG welder needs acceptance checks for the controls that the operator will actually use. Verify parameter meanings, remote behavior and interface documentation as one system. A feature appearing in a catalogue does not establish that it is included in the quoted variant or compatible with your equipment.
Check the controls as delivered
Record peak current, background-current definition, pulse frequency and pulse-time setting where available. Confirm units and whether a percentage refers to peak current or time. Save a trial setting, power down according to the manual, then confirm the intended recall behavior without assuming every model stores the same information.
Use the pulse-current and frequency guide to prepare the parameter record. The procurement decision should compare repeatable behavior on the chosen joint rather than selecting the widest pulse-frequency range. A feature that the procedure never uses should not outweigh a mandatory function that fails.
Require an interface description
For a pedal, finger control, feeder or automation cell, request the correct connector, pin assignment, signal type and compatible accessory reference. Have an authorized integrator approve the connection before use. Do not connect matching-looking plugs or assume that a native remote socket provides a robot interface.
Confirm Torch, Cooling and Gas-System Compatibility
Accept the welding package with the torch, cable length, cooling arrangement and gas controls that will ship. A power source can pass a short demonstration while an underspecified torch or unsuitable connection limits production. System acceptance should identify the weakest rated component and every accessory excluded from the price.
Inspect the delivered connections
Check the torch model, gas and power connections, control plug, work return lead and consumables against the quotation. For water-cooled systems, confirm the specified cooler, coolant instructions, hose routing and required protection functions. Compatibility needs written confirmation for the exact combination rather than a general statement that the machine supports cooling.
Plan a representative cable route and working reach. Tight bends, damaged hoses or an awkward torch can change the trial independently of power-source quality. Include the replacement-part list and the means of identifying connectors, consumables and seals during service.
Keep shielding variables controlled
Verify the gas supply, leak-check method and required timing through the approved procedure. Do not increase flow indiscriminately to compensate for an unidentified problem. If a trial produces inconsistent welds, record gas, electrode preparation, fit-up and surface condition before assigning the fault to the manufacturer.
Build a DC TIG Sample-Acceptance Record
A useful acceptance record connects each requirement to a method, an observation and a release decision. Keep equipment checks separate from weld inspection, and define who approves each. This prevents an attractive bead photograph from replacing evidence for input compatibility, control behavior or the agreed production configuration.
Use an evidence register
| Acceptance item | Evidence to retain |
|---|---|
| Configuration identity | Serial number, input variant, revision and accessory list. |
| Starting and regulation | Trial sequence, settings, observed faults and agreed limits. |
| Production load | Relevant rating evidence and approved application-trial record. |
| Remote and pulse functions | Parameter definitions, compatible controls and observed behavior. |
| Representative weld | Coupon identity, procedure, inspection method and result. |
| Release decision | Open deviations, corrective action, approver and document revision. |
Agree outcomes before shipment
Use pass, conditional acceptance and fail with explicit definitions. Conditional acceptance must state the remaining restriction, owner and closure evidence. Safety concerns and unmet mandatory requirements should stop release; a low price cannot offset them. Do not treat an unresolved item as approved simply because a delivery date approaches.
Photograph the setup and coupon identification without presenting an illustration as a measured result. Keep raw observations alongside the summary. If a correction changes hardware or software, identify the new revision and repeat the affected checks before approving it.
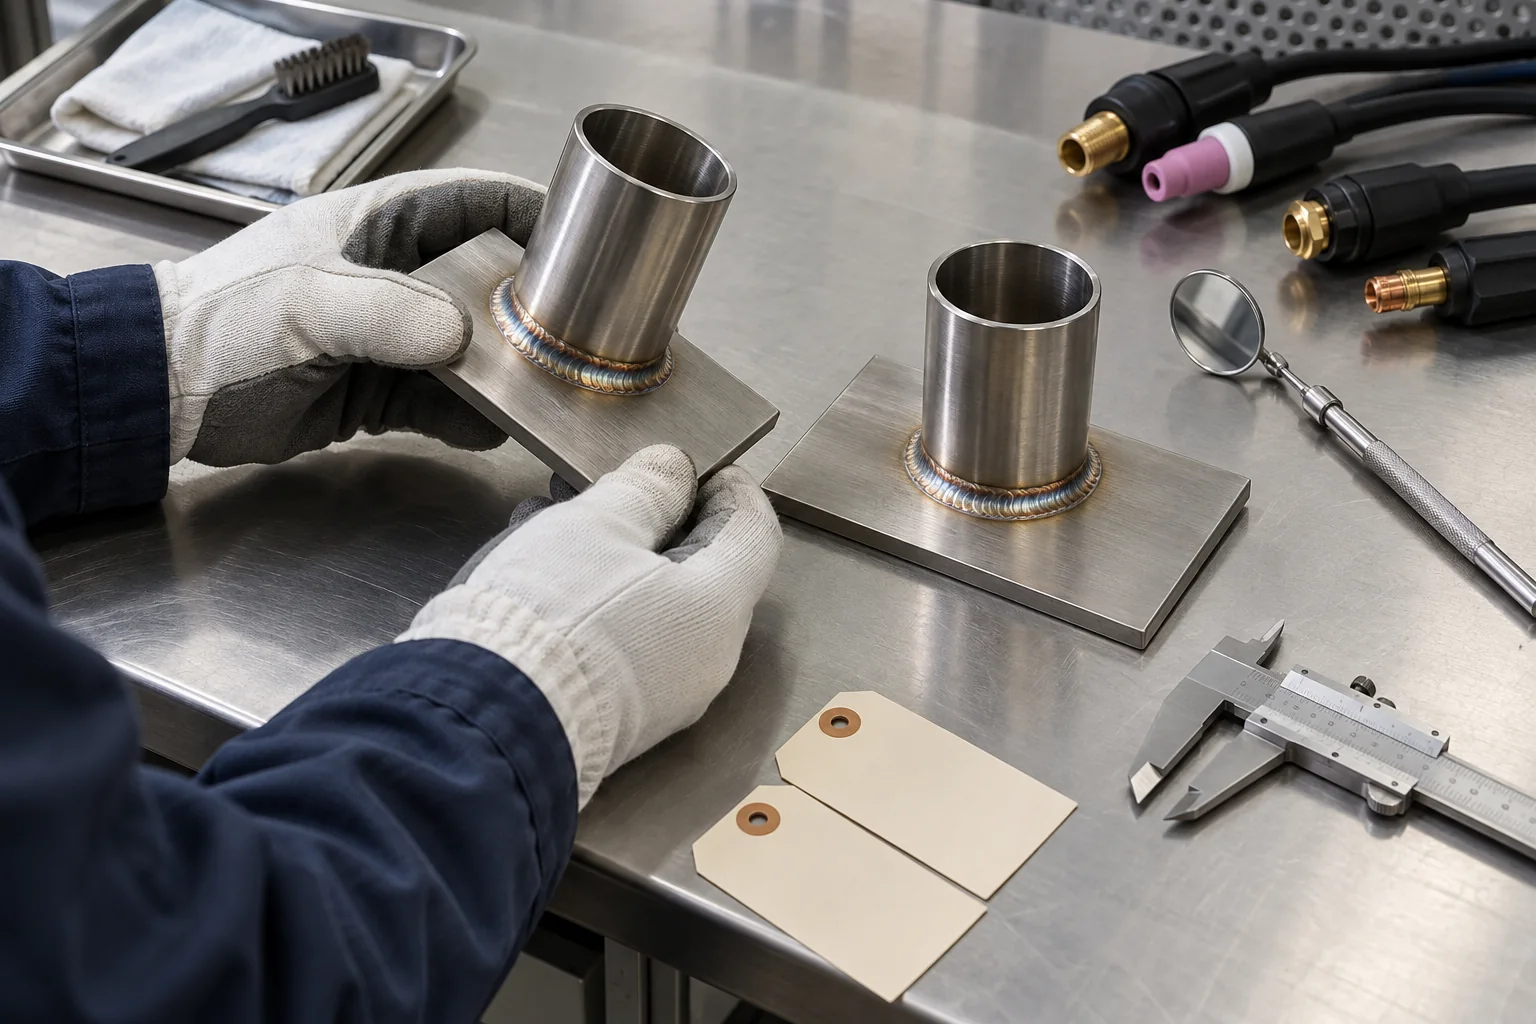
AI-generated illustration of coupon inspection; no acceptance result or measured performance is represented.
Which Factory Documents Support Batch Consistency?
Request documents that connect the approved sample to routine production. The supplier should explain incoming checks, final testing, serial traceability and change notification for the quoted model. This is more useful than collecting certificates whose scope, product identity or issuing organization cannot be matched to the order.
Distinguish type evidence from order inspection
The IEC 60974-1 scope covers safety and performance requirements for industrial and professional welding power sources. Ask which applicable standard and edition the supplier used and request model-specific supporting records. This guide does not assert that GWELD or any listed product has a particular certification.
Ask the responsible technical team to identify the relationship between the tested design, current production revision and destination-market documentation. A commercial sample-acceptance report is not a substitute for conformity assessment or a complete type-test report. Qualified specialists should review the applicable requirements for the market and installation.
Control the move from one sample to a batch
Agree the final-test record format, serial-number linkage and handling of nonconforming units. Require approval for changes that affect fit, function, documentation or service compatibility. Choose pilot-order inspection and sampling with the quality team, rather than inventing a universal sample size for every shipment.
Prepare a Configuration-Specific Request to GWELD
Ask GWELD to match a documented application to a quoted configuration, then confirm the sample plan before committing to volume. The request should identify the required DC capability and all supporting equipment. Keep model-specific evidence, commercial scope and unresolved engineering questions visible in the response.
Send a compact RFQ package
-
- Attach the material list, thickness range and representative joint drawings.
- State input supply, expected current window and production sequence.
- Specify starts, pulse controls, remote functions and required accessories.
- List sample-acceptance checks, inspection responsibilities and open questions.
- Request itemized equipment, sample, spare-part and delivery pricing.
- Identify the destination market, order forecast and required documents.
Start with the published GWELD industrial DC pulse TIG range and request the current model sheet for the exact input and output variant. Alternative AC/DC models may suit mixed-material workshops, but their inclusion below does not make them DC-only products or prove a particular configuration is suitable.
Close the technical gaps before comparing totals
Review the deviation list with purchasing, engineering and quality together. Request a corrected quotation when the sample needs an additional cooler, different torch or interface option. Send the completed application sheet to the GWELD equipment inquiry team for a matched proposal; this guide does not promise a price, lead time or guaranteed welding outcome.
Related Products

TIG 180/200/225 DC Pulse
A compact, air-cooled TIG/Stick inverter welder designed for AC and DC welding.
- Built with durable internal components and a reinforced structure for long-term reliability.
- Supports TIG Pulse and Stick welding across stainless steel, carbon steel, copper, and other common metals.
- Compact and portable design for workshops, garages, mobile repair, and everyday fabrication work.

TIG 300/400/500 DC Pulse
A compact, air-cooled TIG/Stick inverter welder designed for AC and DC welding.
- Uses stronger and more durable material
- Water Cooler compatible.
- Equipped with selected and reliable accessories to enhance the welder’s experience.
- Industrial level welder with a higher redundancy design increases reliability, extends service life, and enhances durability.
TIG 180/200/225P ACDC
A compact, air-cooled TIG/Stick inverter welder designed for AC and DC welding.
- Designed for aluminum welding, with precise control for thin and delicate materials.
- Advanced pulse technology helps reduce heat input and improve weld appearance.
- Built with durable components and a rugged structure for long-term reliability.
Related Solutions

General Fabrication
The ultimate TIG welder solution for diverse fabrication needs. Built with solid materials and thoughtful R&D, our machines offer the precise control required for stainless steel and the reliable power for carbon steel. Experience professional performance in a balanced design engineered for the versatile fabricator.

Heavy Fabrication
The ultimate TIG welder solution for heavy-duty industrial demands. Built with solid materials and thoughtful R&D, our machines offer the precise control required for high-integrity stainless steel joins and the reliable power needed for deep penetration in thick carbon steel. Experience professional performance in a balanced design engineered for the most demanding fabrication environments.

Pipeline
The ultimate TIG welder solution engineered for critical pipe fabrication and field pipeline construction. Driven by thoughtful R&D and built with heavy-duty solid materials, our machines deliver the precise arc control required for flawless 5G/6G root passes on stainless steel and the reliable power for deep-penetration fill passes on carbon steel pipes. Achieve X-ray quality joints and maximum uptime with a balanced design built for the world’s most demanding energy and process piping projects. GWELL ensures your crew is always ready to go with professional performance that eliminates costly field rework.
Frequently Asked Questions
Conclusion
Choose a DC TIG welder manufacturer by connecting a real application to an identified sample and a documented acceptance decision. Confirm process suitability, input supply, low-current starts, relevant duty-cycle evidence, controls and the complete torch-and-cooling package. Retain the observations and resolve mandatory deviations before releasing a batch.
Carry the approved configuration into production through serial records, final-test documentation and controlled changes. For a project-specific review, send your material, joint, electrical supply and equipment requirements through the GWELD technical quotation form. Request the evidence needed for your order rather than assuming that a broad product claim covers every model.