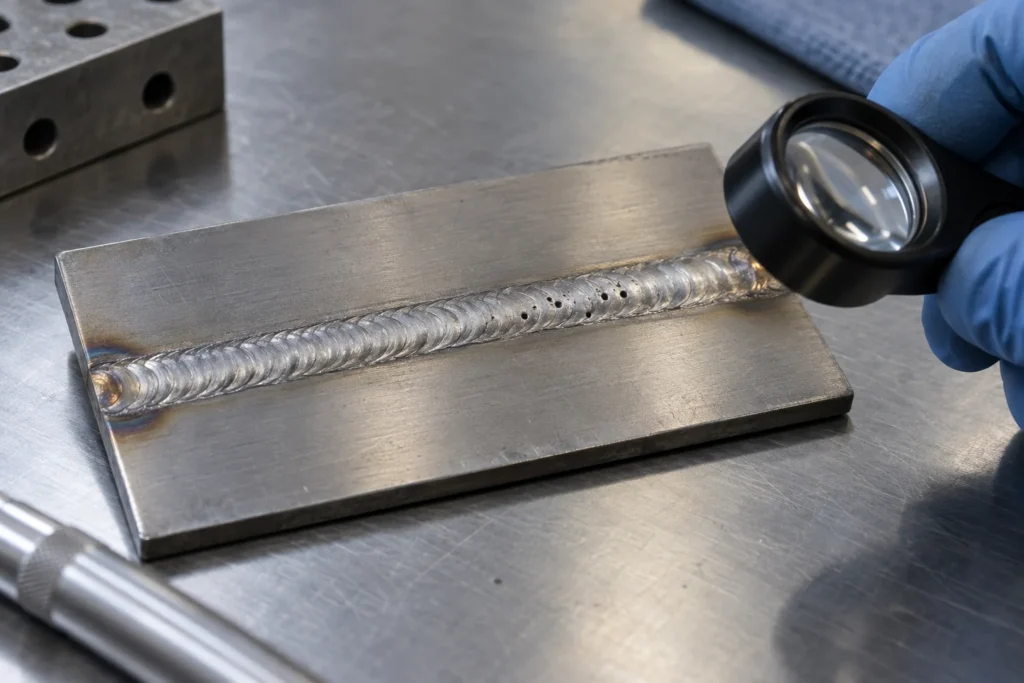
TIG Back Purging: Stainless Steel Pipe Setup and QC Guide
Introduction
TIG back purging protects the reverse side of a weld with a controlled gas atmosphere. For stainless steel pipe fabrication, the practical challenge is to connect that protection with a repeatable setup, a documented monitoring method and the project's inspection requirements.
This guide helps fabrication managers, welding engineers and industrial buyers organize that work. It separates torch shielding from root protection, explains the information a purge setup record should contain and shows how to turn production requirements into an equipment inquiry. It does not prescribe universal flow rates, oxygen limits or acceptance criteria. Those decisions belong to the applicable procedure and responsible engineering and quality personnel.
What Is TIG Back Purging?
Distinguish the three protection zones
Torch shielding protects the weld pool from the welding side. Back purging supplies gas to the root side. A trailing shield extends protection over a cooling surface. These are different functions, even when a work cell uses the same gas supply. Linde's weld purging overview describes these distinctions and the importance of atmosphere control.
For a pipe joint, draw the complete arrangement before discussing settings. Mark the torch circuit, purge inlet, outlet, contained volume and sampling point. A simple sketch gives purchasing, maintenance and production a common reference. It also reveals whether two people are using the word shielding to describe different parts of the system.
Define the boundary of this guide
A purge arrangement is part of a welding process, not a substitute for one. The following sections provide a planning and recordkeeping framework. They do not approve a particular alloy, joint, gas mixture or production parameter. Use the approved welding procedure, equipment instructions and inspection plan when deciding whether a proposed arrangement can be used.
Keep the broader TIG welding gas and flow-rate guide available for torch-side discussions. A torch flow indication should not be copied into the purge setup record as evidence of root protection.
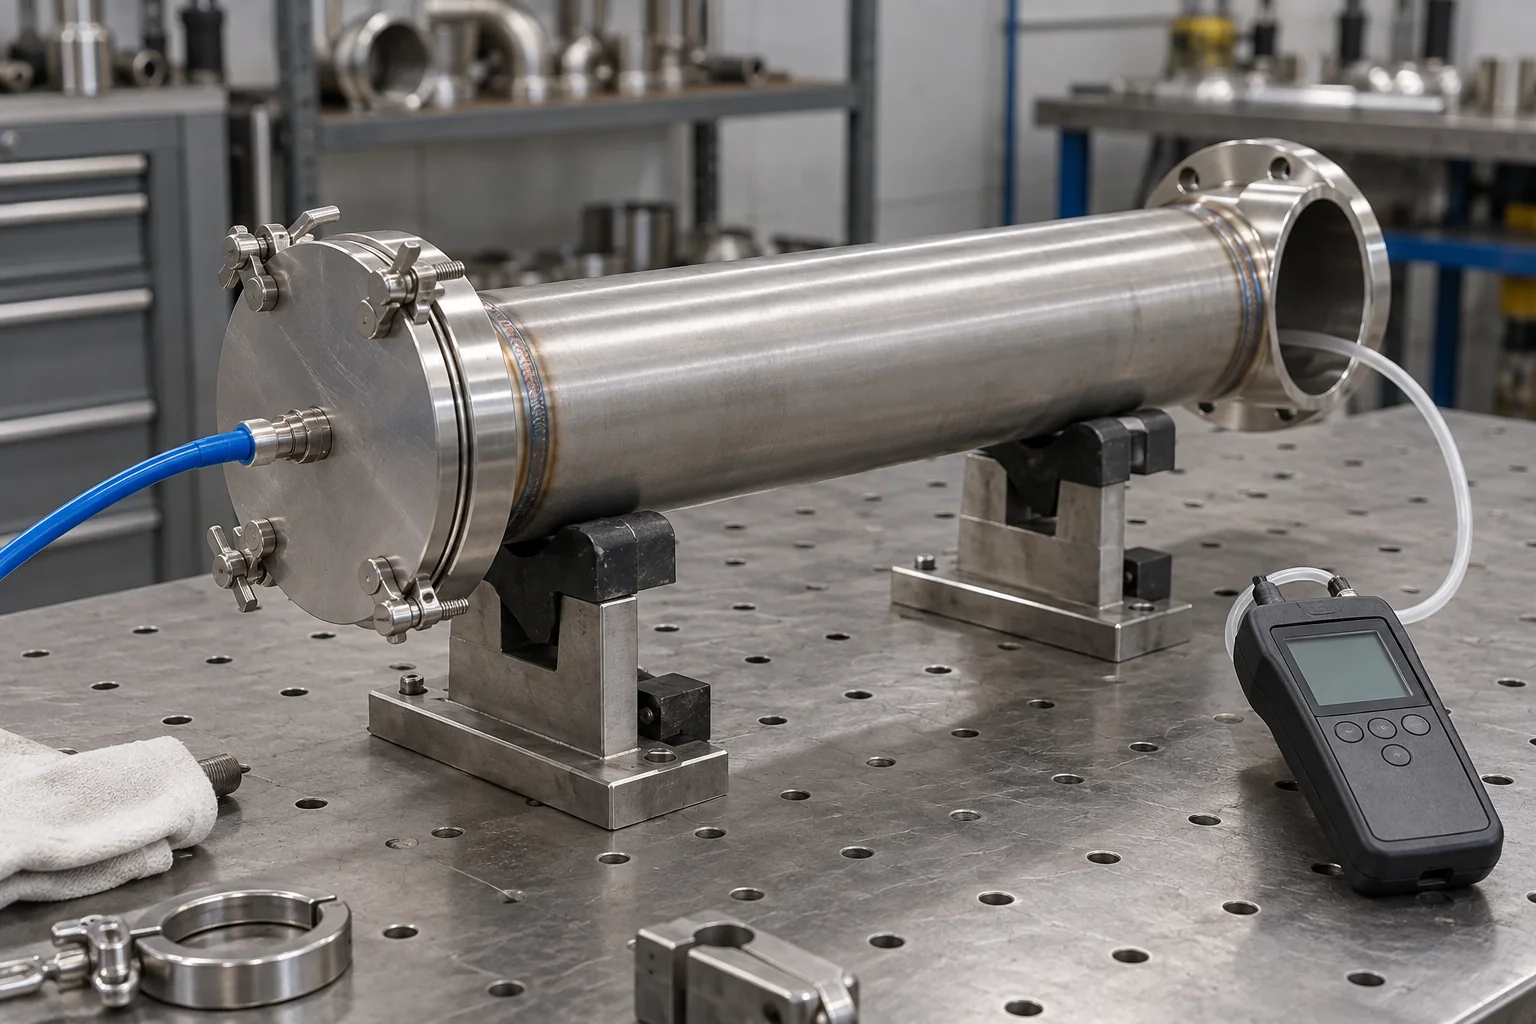 AI-generated generic planning illustration, not an approved installation drawing or customer case.
Start with the Pipework and Inspection Requirements
Collect the application facts
Before specifying stainless steel back purging, identify the material grade, pipe dimensions, joint geometry and service environment. Include the workpiece drawing revision and the location of the weld. A request that says stainless pipe only leaves important differences unresolved, particularly when the inside surface will be inaccessible after assembly.
Record which team owns procedure approval and which team owns inspection release. Ask whether the project requires internal examination, photographs, traceable monitoring records or additional testing. Do not translate a customer's general request for a clean weld into an invented acceptance standard.
Keep procedure changes under control
Miller's stainless tube and pipe guidance identifies root protection as an important consideration and states that qualified procedures require proper qualification processes when modified.
Create a short requirements sheet for the application. Separate mandatory conditions from preferences and open questions. Assign an owner and due date to every unresolved item. For example, an unconfirmed inspection method should remain a visible question rather than quietly becoming a visual-only check during a sample demonstration.
- Material and joint identification.
- Procedure and drawing references.
- Required monitoring and inspection evidence.
- Named approval and release responsibilities.
Separate Torch Gas from the Root Purge Circuit
Label the complete gas path
A useful TIG purge setup record identifies the supply connection, regulator, metering device, hoses and fittings used for each circuit. Draw each path through to its final destination. Where equipment is shared, make the arrangement explicit so a later operator does not assume that adjusting one indication controls both torch and root protection.
Give the two circuits clear names in the work instruction. Use those same names in the sample report, purchasing request and maintenance checklist. Consistent naming helps reviewers distinguish an observed torch-side problem from a change to the internal purge arrangement without relying on memory.
Record the installed condition
Document the installed components and their identification, not just the list from the quotation. Photograph the arrangement when permitted by the job and keep the image with the work-cell record. A replacement fitting, different hose route or moved measuring point should trigger the review required by the plant's change process.
If the team also needs to review front-end consumables, use the TIG gas lens fit and procurement guide. A gas lens belongs to the torch-side configuration. It does not replace a separately required root purge or prove that the inside of the pipe meets its atmosphere requirement.
Plan Containment, Venting and Access
Make the arrangement reproducible
For planning purposes, identify the boundaries of the volume being purged and the approved means of containing it. Record the position and reference of any dams, end closures or fixtures. Include access restrictions and how temporary items will be accounted for after the operation. A later shift should be able to recognize the arrangement from the record.
The inlet, outlet and sampling arrangement must follow the approved design and supplier instructions. Do not create a sealed pressure vessel by improvising closures. Have the responsible personnel review venting and safe operating conditions before any gas is introduced. An illustration in this article is not an installation drawing.
Plan the removal and handover steps
Containment equipment can become a production-control issue when responsibility for installation and removal is unclear. Assign both steps to named roles. Specify how the completion record confirms that temporary equipment has been removed or remains installed only where the job explicitly permits it.
Include a handover note for interrupted work. State the joint status, installed arrangement and checks that must be repeated before restarting. Do not assume that an earlier satisfactory result remains valid after a break, a repositioned workpiece or an opened connection. The responsible team should define the restart checks within the work instruction.
Select Purge Gas through the Approved Procedure
Avoid a universal gas recommendation
Argon is commonly discussed for stainless steel TIG root protection. However, the correct gas or mixture depends on the material and applicable procedure. Linde describes different purge gas options and material-dependent selection. That breadth is a reason to confirm the specific application, not permission to substitute gases without review.
Ask the gas supplier and welding engineer to confirm the specified composition, supply documentation and handling requirements. Do not assume that a familiar cylinder color identifies the contents in every country. Keep the actual gas identification with the sample and production records.
Make the purchasing description precise
The procurement request should state the approved gas reference and the evidence needed on delivery. Include compatible supply connections, metering requirements and the person responsible for installation review. Keep recurring consumables distinct from equipment so the purchase order does not accidentally omit a required supply item.
Changes to supply arrangements should be visible in the change record. A different vendor, cylinder package or connection method may require review even if the headline gas description is unchanged. Ask the responsible team which checks apply rather than declaring every substitution equivalent.
For general process context, see the stainless steel TIG pipe and pulse guide. Keep that overview separate from the application-specific approval documents.
Specify Oxygen Monitoring without Inventing a Limit
Identify the measurement requirement
When the job requires purge oxygen monitoring, define the instrument, measurement range, sampling arrangement and applicable verification requirements. Record where the sample is taken and how the reading is linked to the joint. A displayed value without that context is difficult to compare across shifts or different setups.
This guide does not assign a universal oxygen threshold. The responsible engineering and quality team must define the relevant limit, measurement method and decision rule for the actual material and service. Keep those references beside the recorded result so reviewers can understand why an operation was allowed to proceed.
Record results in a usable format
Include instrument identification, verification status, sample location, units, date, time and operator in the monitoring record. State what to do if a result is unavailable, unstable or outside the approved condition. A missing reading should remain missing rather than being replaced by a previous result or an assumed zero.
Define whether the application needs a startup check, continued observation, periodic recording or a different method. This decision should come from the job requirements. Avoid turning an illustrative checklist into an unauthorized monitoring schedule. Retain the approved record format with the procedure revision so changes are traceable.
Use a Purge Setup Record for Every Representative Trial
Link settings to the actual arrangement
A TIG back purging checklist should connect configuration, measurement and outcome. Keep the units shown on each device and identify whether a recorded number is a setting, a reading or an approved limit. Do not mix those three meanings in one unlabeled column.
| Record field | What to identify | Why retain it |
|---|---|---|
| Joint and material | Drawing, grade and weld reference | Connect the result to the work |
| Purge arrangement | Inlet, outlet, containment and sample point | Reproduce the installed configuration |
| Gas supply | Approved gas and supply identification | Check delivered configuration |
| Monitoring | Instrument, units and verification status | Interpret the reading correctly |
| Decision | Procedure reference and authorized reviewer | Keep approval traceable |
Keep revisions together
Retain the setup drawing, procedure reference, sample results and review decision as one package. A trial photograph saved separately from its configuration record can lose much of its usefulness. Use a stable trial identifier on each item and identify which revision the reviewer accepted.
If several departments participate, assign one person to assemble the completed package. This is an administrative responsibility, not authority to approve a weld. Keep the technical sign-off with the designated personnel while making the evidence easy to retrieve for production and future purchasing.
Investigate Root Discoloration with a Controlled Review
Describe the finding before naming its cause
Record the location, inspection method and appearance of a root-side finding. Keep a suspected shielding problem separate from a confirmed cause. Miller's common TIG problem guide discusses oxygen exposure and stainless root sugaring. That general relationship does not identify the cause of every production indication.
Preserve the original setup and recent change history before replacing components. Ask which joints and production periods require containment or review. A troubleshooting exercise should not quietly release suspect parts because the newest sample appears cleaner.
Compare one planned change at a time
Write down the hypothesis, planned change and evidence expected from the trial. Keep the remaining conditions documented. If several changes are necessary together, state that the result cannot isolate a single cause. The report should show what the comparison establishes and what remains uncertain.
Use the TIG welding porosity investigation guide when gas cavities are part of the finding. Root discoloration and porosity should not be treated as interchangeable observations. Let qualified personnel classify the indications and decide the appropriate inspection and disposition.
Review Internal Inspection and Production Release
Agree on access before the demonstration
A sample demonstration should use an inspection plan agreed before welding. Identify whether the root will be examined directly, with a suitable viewing instrument, after sectioning a sample or by another required method. Record access limitations so the report does not imply that an unobserved region was inspected.
Photographs and video can support a review, but their purpose and limits should be stated. Include the joint identification and viewing location. Keep training illustrations separate from actual production evidence. A bright-looking image alone cannot certify corrosion performance, dimensions or compliance with the full project specification.
Separate completion from acceptance
Use explicit statuses in the record. Trial completed, inspection completed, action required and released are different states. Name the person responsible for each decision and retain the applicable report. This avoids treating a completed demonstration as an automatic production approval.
| Stage | Evidence to retain | Decision owner |
|---|---|---|
| Setup review | Arrangement and procedure reference | Designated engineering personnel |
| Trial completion | Actual configuration and monitoring record | Trial coordinator |
| Inspection | Required examination and findings | Authorized inspection personnel |
| Disposition | Acceptance basis and action decision | Designated quality authority |
| Production transfer | Approved instructions and training record | Production and quality roles |
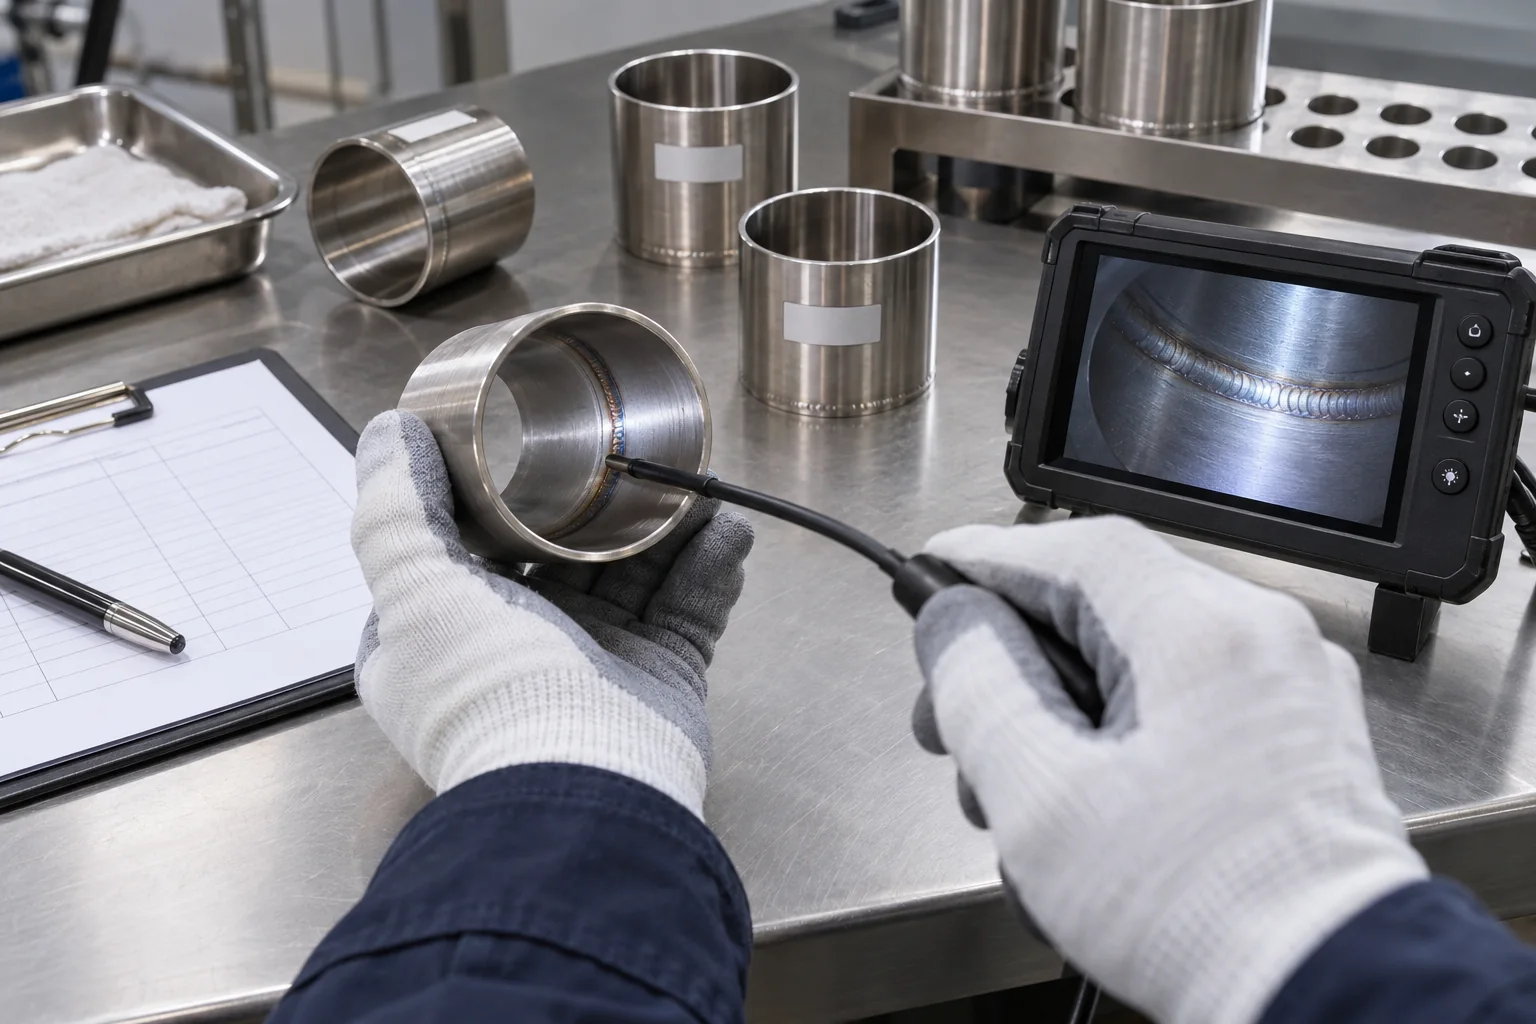 AI-generated inspection illustration; actual acceptance follows the project's approved examination and release process.
Turn Purging Requirements into an Equipment Inquiry
Specify the complete work-cell requirement
An equipment inquiry should describe the material, joint, production method and approved process requirements. Include the planned torch, control method, cooling arrangement and accessory interfaces. State whether the supplier is being asked for a power source only or a defined work-cell package with separately listed responsibilities.
Review the GWELD TIG equipment range for the power-source discussion. Confirm each required feature on the actual model and configuration quoted. Do not assume that a machine includes a purge controller, oxygen analyzer or complete pipework tooling unless those items are explicitly listed and confirmed.
Ask for evidence with the quotation
Request a configuration list, interface documentation, applicable operating instructions and an agreed demonstration plan. Identify any buyer-supplied equipment and the checks needed before integration. Keep spare parts, training, delivery and support commitments in writing rather than relying on a general product-family description.
- Part, material and production requirements.
- Power-source, torch and accessory configuration.
- Interfaces and separately supplied monitoring equipment.
- Sample demonstration and inspection responsibilities.
- Documentation, spares and support scope.
Send the application sheet to the GWELD team for a matched TIG equipment proposal. Define what the proposal must answer before comparing prices.
Plan Handover, Maintenance and Gas Safety
Keep the approved arrangement recognizable
After a successful review, transfer the accepted configuration into the plant's controlled instructions. Identify permitted replacements and the changes that require engineering review. Keep component references and installed photographs accessible to maintenance so a repair does not unintentionally create a different work-cell arrangement.
Use the same trial and joint references when discussing recurring problems. Compare records from accepted and affected production periods, and keep estimated costs separate from measured downtime, inspection and rework costs. This makes the commercial discussion more useful than a claim that a new accessory always saves a fixed percentage.
Include the gas-risk assessment
Linde notes the increased asphyxiation risk associated with purge gas use. Have qualified site safety personnel determine ventilation, gas handling and monitoring requirements for the location. This article does not authorize work in a confined space or replace the site's permit and emergency arrangements.
Do not begin a demonstration while safety responsibilities remain unresolved. Keep the risk assessment, equipment instructions and approved work method available to the team. Include the removal, isolation and handover steps in the planning review so completion of welding is not mistaken for completion of the whole task.
Related Products

TIG 300/400/500 DC Pulse
A compact, air-cooled TIG/Stick inverter welder designed for AC and DC welding.
- Uses stronger and more durable material
- Water Cooler compatible.
- Equipped with selected and reliable accessories to enhance the welder’s experience.
- Industrial level welder with a higher redundancy design increases reliability, extends service life, and enhances durability.

Welding Gas Flow Meter Regulator
Dual-stage gas flow meter regulator with accurate flow control for Argon and CO2 shielding gas applications.
- V SERIES uses stronger and more durable material, increasing the service life of the welder.
- Can weld stainless steel, copper, carbon steel, alloy steel, cast iron, and more.
- Lightweight and portable, adaptable to various environments.
TIG Welding Torch WP-17 Series
High-quality TIG welding torch with flexible cable and ergonomic handle design for professional welding applications.
- V SERIES uses stronger and more durable material, increasing the service life of the welder.
- Can weld stainless steel, copper, carbon steel, alloy steel, cast iron, and more.
- Lightweight and portable, adaptable to various environments.
Related Solutions

Pipeline
The ultimate TIG welder solution engineered for critical pipe fabrication and field pipeline construction. Driven by thoughtful R&D and built with heavy-duty solid materials, our machines deliver the precise arc control required for flawless 5G/6G root passes on stainless steel and the reliable power for deep-penetration fill passes on carbon steel pipes. Achieve X-ray quality joints and maximum uptime with a balanced design built for the world’s most demanding energy and process piping projects. GWELL ensures your crew is always ready to go with professional performance that eliminates costly field rework.

General Fabrication
The ultimate TIG welder solution for diverse fabrication needs. Built with solid materials and thoughtful R&D, our machines offer the precise control required for stainless steel and the reliable power for carbon steel. Experience professional performance in a balanced design engineered for the versatile fabricator.

Maintenance & Repair
The ultimate TIG welder solution for unpredictable repair demands. Built with solid materials and thoughtful R&D, our machines provide the precise arc control needed for delicate stainless repairs and the reliable power for rugged on-site fixes. Experience professional performance in a balanced design that is compact, portable, and engineered to keep your operations ready to go—no matter the location.
Frequently Asked Questions
Conclusion
TIG back purging should be planned as a documented part of the stainless pipe welding process. Define the application, separate the torch and root circuits, identify the contained volume and monitoring method, and retain the inspection decision with the actual setup record.
When equipment is needed, translate those requirements into a specific configuration and demonstration request. Ask GWELD for an application-based TIG equipment proposal, and confirm the scope of every accessory and interface. Keep procedure approval, gas safety and weld release with the responsible personnel for the job.