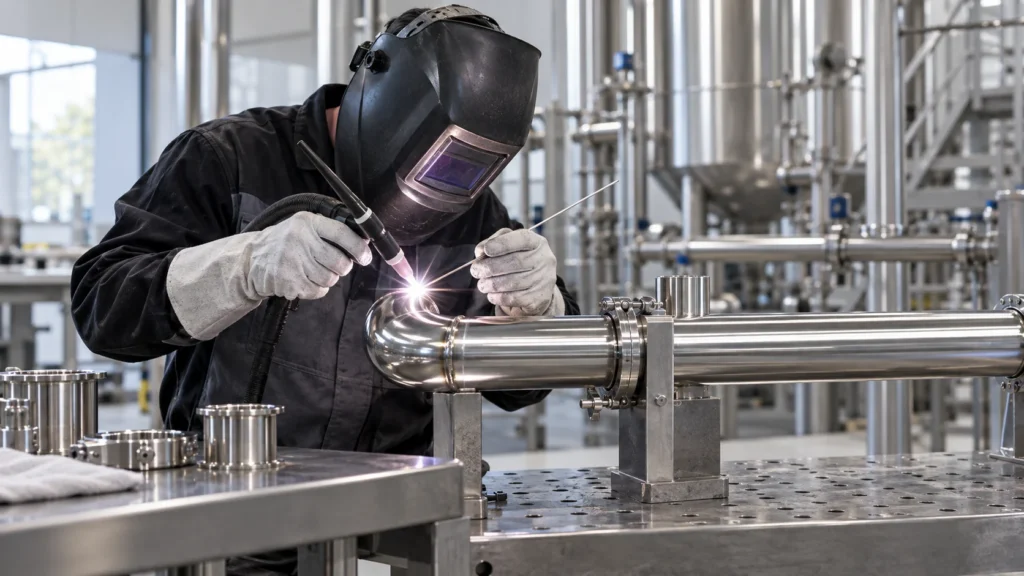
TIG Welding Stainless Steel: Pipe, Pulse & Purging Guide
Introduction
TIG welding stainless steel requires control of heat input, shielding, joint cleanliness and filler selection. DC electrode-negative output and argon shielding are common choices, but final settings must follow the material, joint and qualified welding procedure.
This guide focuses on stainless steel pipe and pulse TIG: how to plan heat control, root protection and a documented setup. If you are selecting equipment, use the stainless steel welding machine buying guide for model-specific procurement checks.
Heat Input, Cleanliness and Corrosion Requirements
Stainless steel weld quality depends on the complete procedure, including material grade, joint preparation, heat input and the required surface condition. Do not treat a clean-looking bead as proof of corrosion performance or code compliance.
Before welding
- Confirm base-metal grade, filler classification and the applicable procedure.
- Keep preparation tools and consumables free from carbon-steel contamination.
- Control fit-up, arc length, travel and weld sequence; measure interpass temperature where required.
- Define heat-tint, inspection and post-weld treatment acceptance criteria before production.
TWI’s heat-tint guidance explains why weld oxidation needs consideration alongside corrosion requirements. Select any cleaning process against the job specification.

Pulse TIG Settings: What to Record and Validate
Pulse TIG alternates peak and background current. Frequency, peak-time fraction, current levels and travel speed work together; increasing frequency alone does not guarantee lower distortion or faster output.
Record the complete pulse setup
- Machine model, available pulse range and control mode
- Peak current, background current, frequency and peak-time fraction
- Electrode and filler size, joint fit-up and welding position
- Travel speed, acceptance results and heat-input requirements
Compare a controlled sample with the existing approved process. Use the pulse TIG manufacturer buying guide to request model-specific control and factory-test evidence.
Stainless Steel Pipe Back Purging and Root Protection
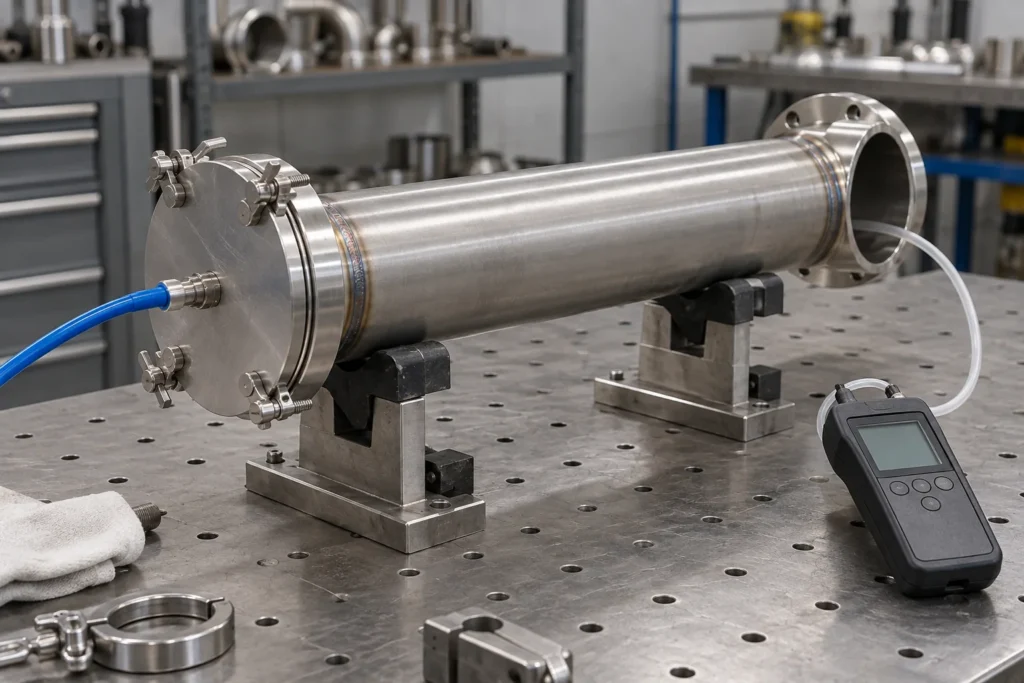
Back purging protects the hot root of a stainless steel pipe weld where the procedure requires it. Seal the purge zone, provide an appropriate vent and verify gas delivery rather than relying only on elapsed purge time.
Use project-specific acceptance limits
Required residual oxygen, purge duration and inspection criteria depend on the alloy, service, joint and project specification. There is no single oxygen threshold that proves compliance for every stainless steel pipe job.
- Confirm purge gas, fixture arrangement, leakage control and monitoring requirements.
- Maintain protection through the stages specified by the welding procedure.
- Record the root condition and required inspection results before scaling production.
Review Miller’s stainless tube and pipe guidance and our TIG shielding gas guide for setup considerations.

Stainless Steel TIG Setup Record: Procedure Checklist
This chart is a documentation checklist, not a verified amperage recipe or a substitute for a qualified welding procedure.
| Setup item | Record before production | Approval check |
|---|---|---|
| Material and joint | Grade, thickness, fit-up and welding position | Match the qualified procedure and service requirements |
| Power source | Model, polarity, current and pulse controls | Confirm actual available modes and output evidence |
| Consumables | Tungsten classification and filler specification | Check identification, diameter and traceability |
| Gas shielding | Gas type, torch flow, cup and root protection | Validate coverage and project-specific purge criteria |
| Thermal control | Travel, sequence and interpass checks | Stay within procedure requirements |
| Inspection | Acceptance method and sample results | Obtain the required engineering approval |
Use our stainless steel TIG filler selection guide alongside the electrode and machine documentation.
How to Compare Continuous and Pulsed TIG
Compare processes on representative parts under controlled conditions. Pulse is an option to evaluate, not an automatic quality guarantee.
| Evaluation | Continuous DC TIG | Pulsed DC TIG |
|---|---|---|
| Controls to record | Current and travel | Peak/background current, frequency, peak-time fraction and travel |
| Quality checks | Required joint and inspection criteria | The same joint and inspection criteria |
| Cost comparison | Accepted output, labor, gas and rework | Accepted output, labor, gas and rework under the trial settings |
Do not infer a fixed distortion reduction, travel-speed gain or NDT success rate from the presence of pulse controls alone.
Illustrative Stainless Pipe Qualification Workflow
This workflow is illustrative; it is not a documented GWELD customer case or a guaranteed production result.
- Agree material, joint, service and inspection requirements with the responsible welding engineer.
- Confirm the machine, torch, filler, gas and root-protection arrangement.
- Document a representative sample, including pulse controls and thermal checks where applicable.
- Assess the sample against the required procedure and acceptance criteria.
- Release a controlled setup record and compare accepted output and rework during production.
Related Products

TIG 180/200/225 DC Pulse
A compact, air-cooled TIG/Stick inverter welder designed for AC and DC welding.
- Built with durable internal components and a reinforced structure for long-term reliability.
- Supports TIG Pulse and Stick welding across stainless steel, carbon steel, copper, and other common metals.
- Compact and portable design for workshops, garages, mobile repair, and everyday fabrication work.

TIG 180/200/225P ACDC
A compact, air-cooled TIG/Stick inverter welder designed for AC and DC welding.
- Designed for aluminum welding, with precise control for thin and delicate materials.
- Advanced pulse technology helps reduce heat input and improve weld appearance.
- Built with durable components and a rugged structure for long-term reliability.
TIG 300/400/500 DC Pulse
A compact, air-cooled TIG/Stick inverter welder designed for AC and DC welding.
- Uses stronger and more durable material
- Water Cooler compatible.
- Equipped with selected and reliable accessories to enhance the welder’s experience.
- Industrial level welder with a higher redundancy design increases reliability, extends service life, and enhances durability.

TIG 315/350P ACDC
A compact, air-cooled TIG/Stick inverter welder designed for AC and DC welding.
- Water Cooler compatible.
- Uses stronger and more durable material.
- Equipped with selected and reliable accessories to enhance the welder’s experience.
- Industrial level welder with a higher redundancy design increases reliability, extends service life, and enhances durability.

TIG 400/500P ACDC
A compact, air-cooled TIG/Stick inverter welder designed for AC and DC welding.
- Water Cooler compatible.
- Uses stronger and more durable material.
- Equipped with selected and reliable accessories to enhance the welder’s experience.
- Industrial level welder with a higher redundancy design increases reliability, extends service life, and enhances durability.
Related Solutions

Maintenance & Repair
The ultimate TIG welder solution for unpredictable repair demands. Built with solid materials and thoughtful R&D, our machines provide the precise arc control needed for delicate stainless repairs and the reliable power for rugged on-site fixes. Experience professional performance in a balanced design that is compact, portable, and engineered to keep your operations ready to go—no matter the location.

Offshore
The ultimate TIG welder solution for the most punishing maritime environments. Built with solid materials and thoughtful R&D, our machines are engineered to withstand humidity and salt spray while delivering the precise arc control required for critical offshore infrastructure. Experience professional performance in a balanced design that remains reliable on floating platforms or remote shipyards—ensuring you are always ready to go when the mission is critical.

Pipeline
The ultimate TIG welder solution engineered for critical pipe fabrication and field pipeline construction. Driven by thoughtful R&D and built with heavy-duty solid materials, our machines deliver the precise arc control required for flawless 5G/6G root passes on stainless steel and the reliable power for deep-penetration fill passes on carbon steel pipes. Achieve X-ray quality joints and maximum uptime with a balanced design built for the world’s most demanding energy and process piping projects. GWELL ensures your crew is always ready to go with professional performance that eliminates costly field rework.
Conclusion: Qualify the Process, Then Select the Equipment
For TIG welding stainless steel, choose equipment that supports the approved procedure and actual production duty. Shielding, filler selection, root protection and inspection remain part of the decision.
Send material grade, wall thickness, joint type, required pulse controls, cooling arrangement and duty pattern to the GWELD equipment consultation team. Request model-specific documentation rather than relying on universal parameter or pass-rate promises.